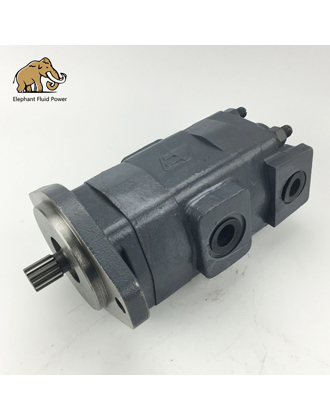
The A11VO for mining dump trucks is a high-pressure variable-displacement piston pump developed by Rexroth for open hydraulic circuits in open-cast and underground mining dump trucks. It is primarily used as the main pump for the lifting system, whilst in some models it also serves as an auxiliary hydraulic power source for steering, braking and cooling. The operating conditions for mining dump trucks are extremely demanding: continuous 24-hour heavy-duty operation, severe jolts and vibrations, high levels of dust, cold starts in winter, and instantaneous high-pressure shocks during lifting and unloading. Thanks to its high-pressure, heavy-duty design, through-shaft series-connection capability, and the optional A11VLO version with an integrated make-up pump, the A11VO has become the mainstream hydraulic power unit for mining trucks ranging from 20 to several hundred tonnes.
First, key technical parameters for mining truck applications
1. Rated continuous pressure: 350 bar; short-term peak pressure: 400 bar, suitable for heavy-load lifting impact pressures
2. Maximum speed: 2,500 rpm for 130/145 specifications; 2,300 rpm for 190/260 specifications; typical operating speed for mining dump trucks is 1,800-2,100 rpm
3. Drive: 100% through-shaft drive; a gear pump may be connected in series at the rear to simultaneously supply the lifting, steering, braking and cooling circuits, thereby simplifying the power take-off transmission mechanism
4. Sub-model distinctions
A11VO Standard Version: Self-priming, commonly used in small to medium-tonnage mining trucks;
A11VLO Enhanced Version: Features a built-in impeller-driven make-up pump to improve oil suction, resist negative pressure and prevent cavitation caused by high speeds and low-temperature, high-viscosity oil; the VLO version must be selected for medium-to-large and large mining dump trucks.
5. Drainage: Dual drain ports; housing drain back pressure is no more than 2 bar; must be drained directly and separately back to the oil tank;
6. Hydraulic fluid requirements: Due to high levels of mining dust, fluid cleanliness must meet ISO 18/15; recommended fluid viscosity is 16-36 mm2/s.
Second, mainstream control methods for mining dump trucks
The vast majority of mining dump truck lifting systems utilise LRDS (LS load-sensing + LR constant power + DR pressure cut-off) composite control, which is the standard configuration for mining dump trucks.
1. LR Constant Power: When lifting under full load, the system automatically reduces displacement as pressure rises, limiting the torque absorbed by the pump and preventing high-horsepower diesel engines from stalling or emitting black smoke; the power setting can be adjusted externally whilst the pump is running to match engines of different horsepower ratings.
2. LS Load-Sensitive: Whilst the vehicle is in motion or in the mid-position during lifting operations, the pump automatically reduces to a low displacement, significantly reducing heat generated by overflow and lowering fuel consumption during prolonged idling in mining operations; during lifting operations, flow is delivered on demand, ensuring smooth and shock-free lifting movements.
3. DR Pressure Cut-off: In the event of instantaneous overpressure upon reaching the limit position during lifting, the pump rapidly reduces to a low displacement, protecting the hydraulic cylinders, pipework and valves, and preventing system damage caused by burst pipes.
Third, Key Advantages of the A11VO for Mining Dump Trucks
1. Shock-Resistant, Heavy-Duty Construction
A thickened cast-iron housing, combined with wear-resistant coatings on the pistons, sliding shoes and distribution plates, withstands the frequent pressure shocks of lifting and unloading operations. With a B10 design life of up to 20,000 hours, it is suited to continuous, all-weather mining operations.
2. Integrated multi-pump system with a common shaft, simplifying the vehicle's drivetrain
The engine's power take-off (PTO) drives the main pump, with gear pumps connected in series via a common shaft at the rear. A single PTO simultaneously supplies the main lifting circuit, the steering circuit and the brake and cooling circuits, thereby reducing the need for a transfer case and lowering the complexity of the vehicle's layout as well as the number of potential failure points.
3. Integrated control for energy efficiency, reducing mining operational costs
The LRDS three-in-one control system automatically reduces displacement during no-load operation. Compared to older fixed-displacement pump systems, this reduces overflow heat generation and fuel consumption by 20-35 per cent, whilst minimising high-temperature failures in the hydraulic system.
4. A11VLO cavitation resistance, suited to harsh mining environments
In open-pit mining, low winter temperatures cause the hydraulic fluid to thicken, whilst underground installations have limited space for oil tank placement. The built-in impeller make-up pump improves inlet negative pressure, suppressing cavitation noise and pitting on the distribution plate, thereby extending the pump's overhaul intervals.
5. Modular valve blocks for easy maintenance and commissioning
The regulator valve block can be removed and installed separately without dismantling the pump core; constant power and cut-off pressure parameters can be adjusted on-site; SAE standard interfaces ensure good interchangeability of spare parts in mining areas.
Fourth, Key Points for On-Site Operation and Maintenance of Mining Trucks
1. Keep the suction line as short as possible with sufficient bore diameter, minimise the number of bends, and reduce suction resistance; high-displacement models must use the VLO make-up pump version.
2. The housing drain line must return independently to the oil tank; it must not be combined with the high-pressure return line, as excessive back pressure may cause seal failure and pump overheating.
3. Due to severe dust in mining environments, strictly adhere to the replacement cycles for hydraulic fluid and filter elements; hydraulic fluid contamination is the primary cause of internal pump wear.
4. Commissioning points: The pressure cut-off should generally be set to 370-390 bar; constant power should be matched to the engine's 90-95 per cent load range to avoid stalling or power wastage.
5. When connecting other pump units in series via a common shaft, ensure coaxiality to prevent damage to the drive shaft caused by excessive radial forces.
 French
 Portuguese
 Russian
 German
 Spanish
 Japanese
 Korean
 Irish
 Greek
 Turkish
 Italian
 Danish
 Romanian
 Indonesian
 Czech
 Afrikaans
 Swedish
 Polish
 Basque
 Catalan
 Esperanto
 Hindi
 Lao
 Albanian
 Armenian
 Azerbaijani
 Belarusian
 Bengali
 Bosnian
 Bulgarian
 Cebuano
 Chichewa
 Croatian
 Dutch
 Estonian
 Finnish
 Galician
 Georgian
 Haitian
 Hebrew
 Hmong
 Hungarian
 Icelandic
 Javanese
 Kazakh
 Khmer
 Latin
 Latvian
 Lithuanian
 Luxembourg
 Macedoniar
 Malagasy
 Malay
 Maltese
 Maori
 Mongolian
 Burmese
 Nepali
 Norwegian
 Pashto
 Persian
 Punjabi
 Serbian
 Sinhala
 Slovak
 Slovenian
 Somali
 Samoan
 Tajik
 Thai
 Ukrainian
 Uzbek
 Vietnamese
 Welsh
 Yiddish
 Yoruba